
Philosophy: factory first
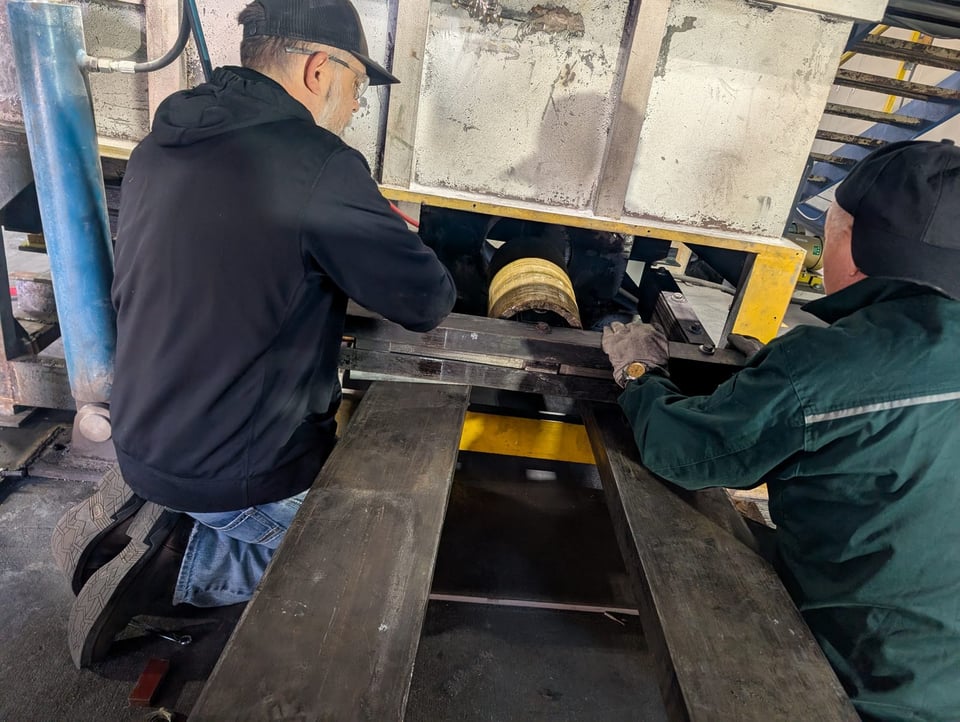
Ameritube exists to answer one question: how do you get consistently American-quality tube at a price the market will pay? The founders' answer was to control the value-adding steps themselves, in the United States, and to test everything. Distribution of complementary alloys came later, and it still plays a supporting role. The factory is the point.
That means:
- In-house control. If a step affects the quality of the tube, we want to do it ourselves and document it.
- Test everything. Every tube sees eddy current. Hard drawing is used deliberately to expose defects.
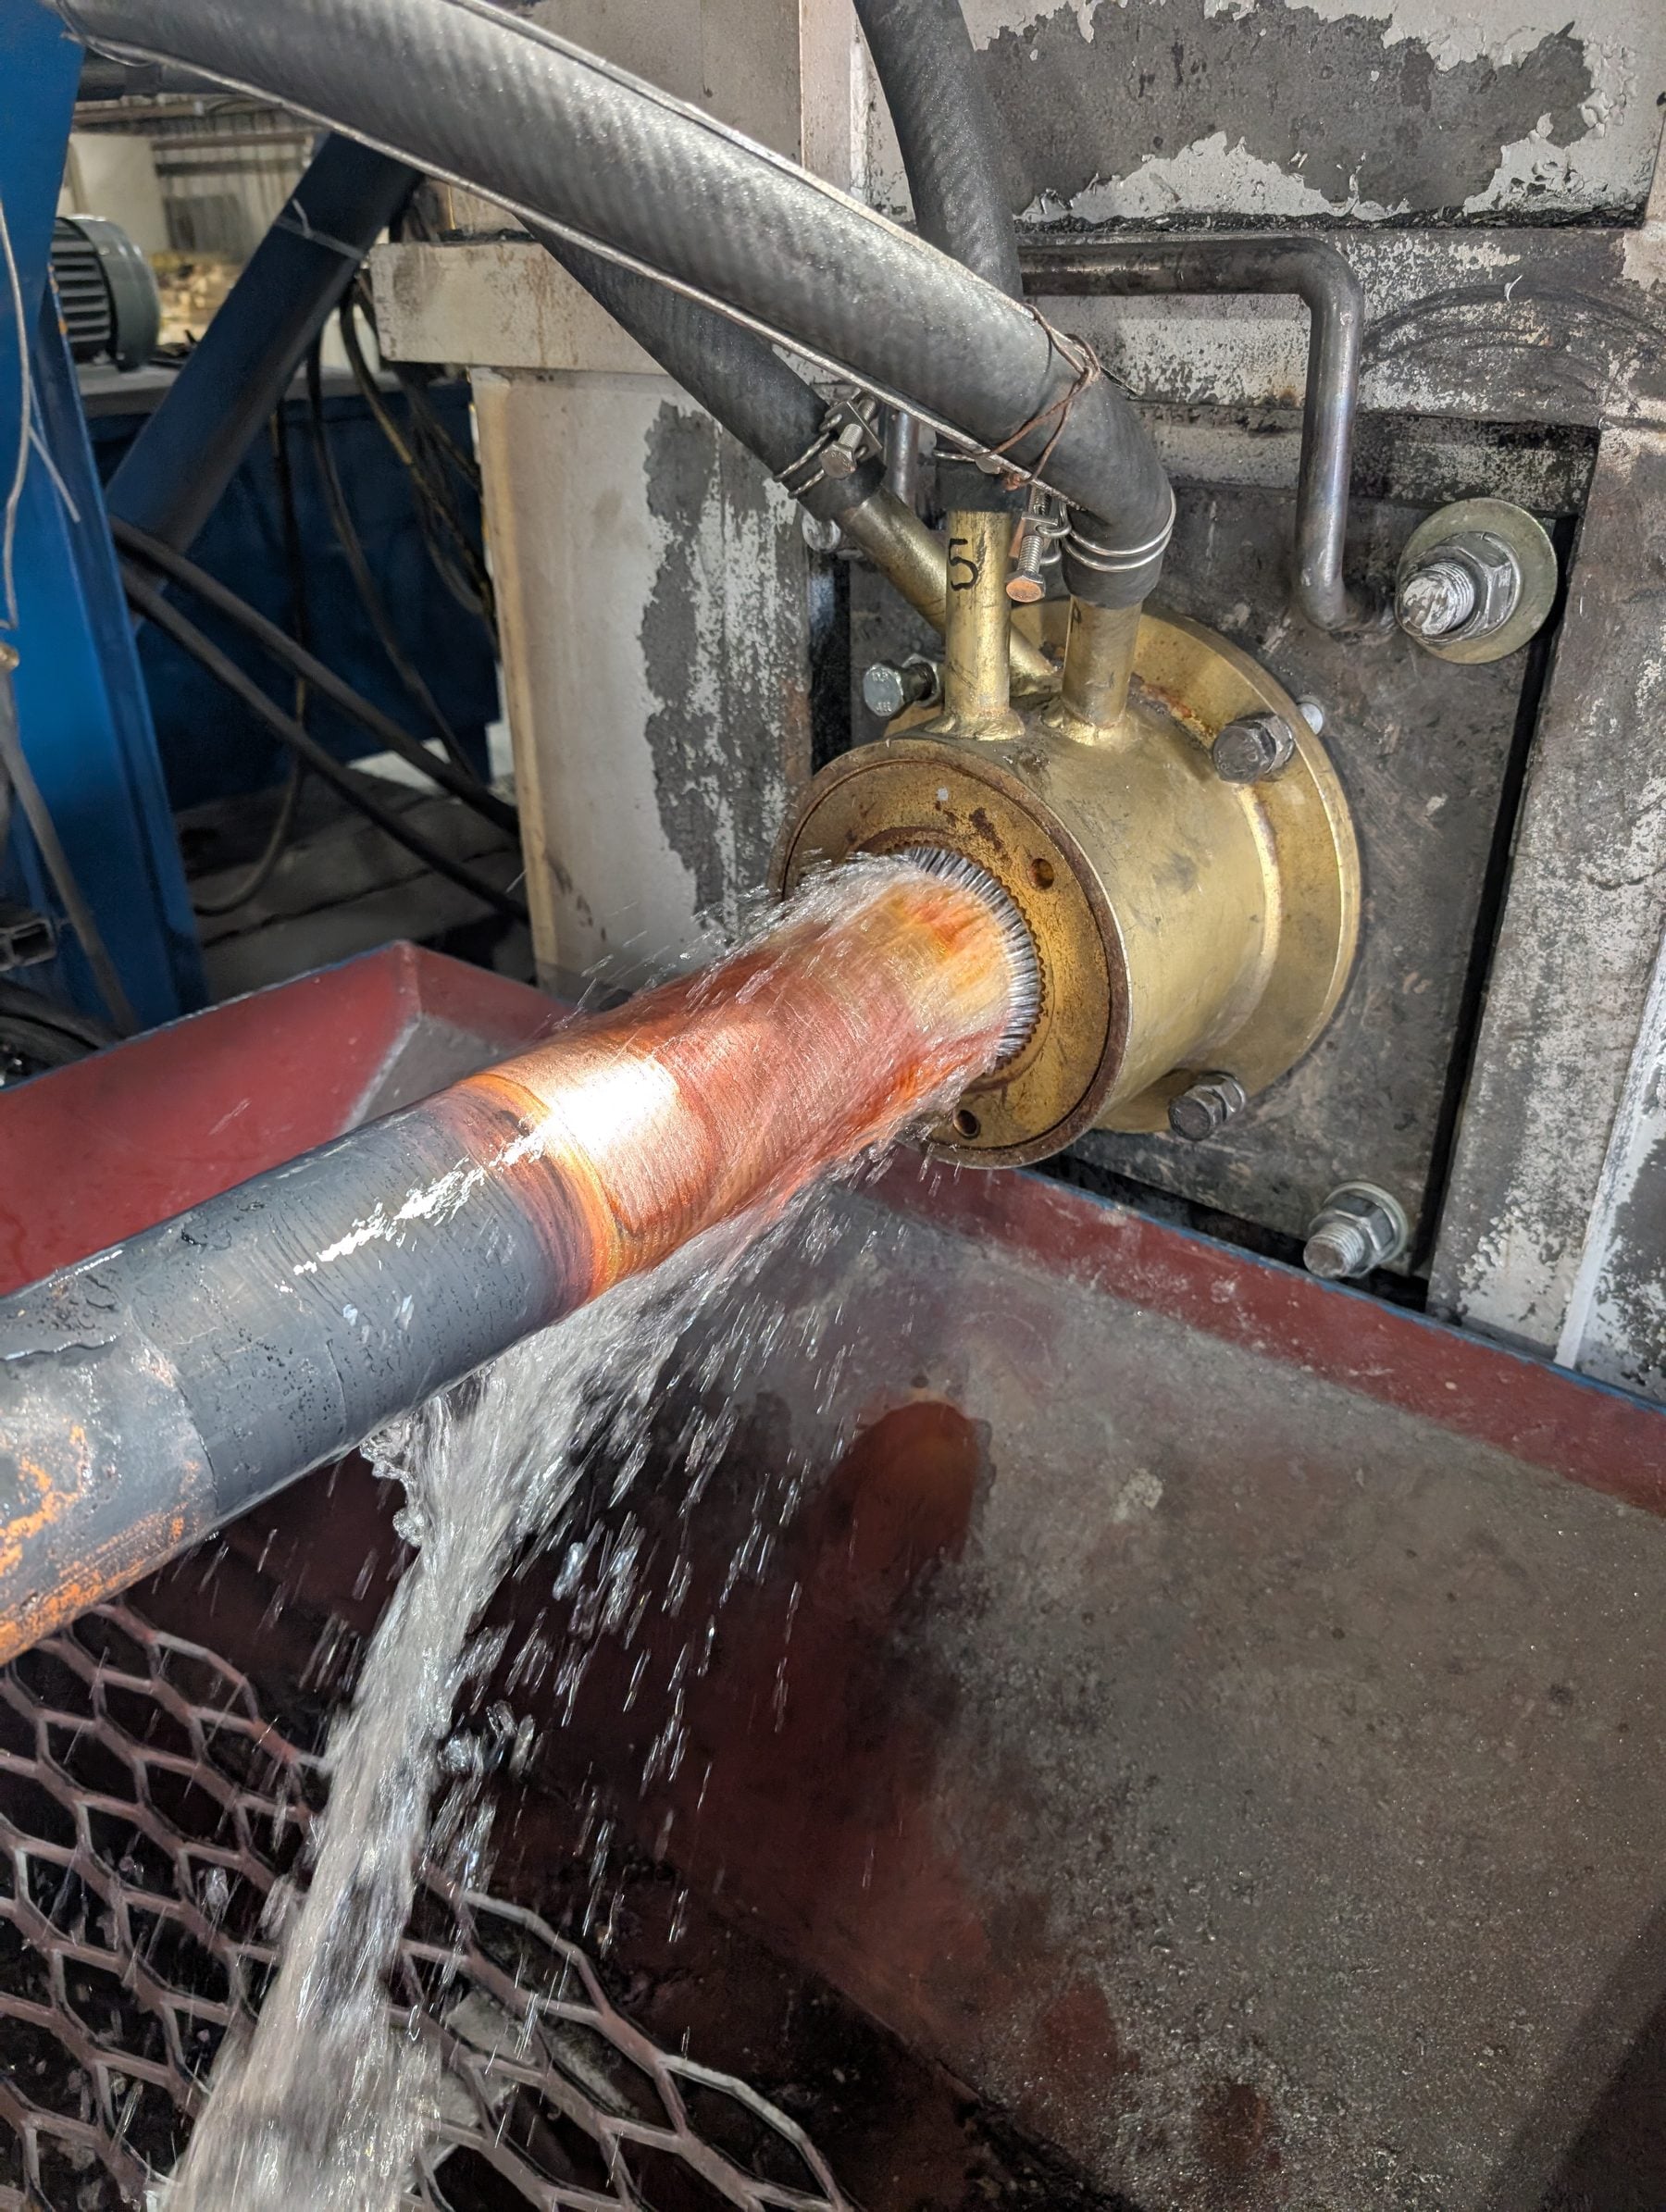
- Made in the USA, and now melting here too. In 2025 Ameritube began melting and casting C12200 copper in-house, the first step toward removing the last dependency on imported hollows. Copper-nickel is next.
- Distribution as a supplement. Carbon, stainless, and nickel alloys are supplied because our customers' jobs need them, and they pass through the same lab before we ship them.
History
- 2004Founded in Hillsboro, Texas
Engineers with patents in steel alloying and years consulting to automakers start with the last step, testing and finishing, so that 100% of what leaves the plant is proven.
- 200712,000 admiralty tubes, zero customer rejections
Four hard draws per tube for ExxonMobil and Petrobras exchangers. Ameritube rejects 1,500 in process. The lesson: overseas raw material needs American processing and American eyes.
- 2008First direct refinery order
C44300 admiralty for a refinery, and C70600 copper-nickel for compressor skid coolers.
- 2011Pilger mill installed
Development of continuous casting technology begins.
- 2012ISO 9001 certified
SOPs, quality processes, and approvals formalised at customer request. Approved for defense and marine work. Stainless and carbon lines added.
- 2013Gulf Coast chemical plants
C70600 and C71500 copper-nickel for plants whose brass bundles kept failing. C71500 approved through third-party ID eddy current testing.
- 2014Hydrostatic and air-under-water testing
Expansion into shipbuilding and artificial lift pump barrels.
- 2015Nuclear tube and a full navy ship set
14,000 C71500 tubes for a Dominion Energy nuclear plant under a customer-surveilled procedure. First complete ship set, with valves, fittings, and flanges, to a foreign navy under FMF. Monel 400 and nickel alloys added.
- 2017 to 2024Nickel line, duplex U-bends, NSF-61 copper
Alloy 200, C-276, 600, 625, 800, 825. Duplex U-bend bundles for Motiva. 18,000 316L U-bends for Praxair. ISO 9001:2015 recertified through March 2027. NSF/ANSI 61 copper plumbing tube launched.
- 2025Melting and casting come in-house
Ameritube melts and continuously casts its first alloy, C12200 copper, in Hillsboro. Melt, cast, pilger, draw, anneal, straighten, and test, in one building. Copper-nickel and brass are next for the furnace.
Where we are
1000 North State Highway 77, Hillsboro, Texas 76645. One hour south of Dallas on I-35, 80,000 square feet of manufacturing, testing, and warehouse.