
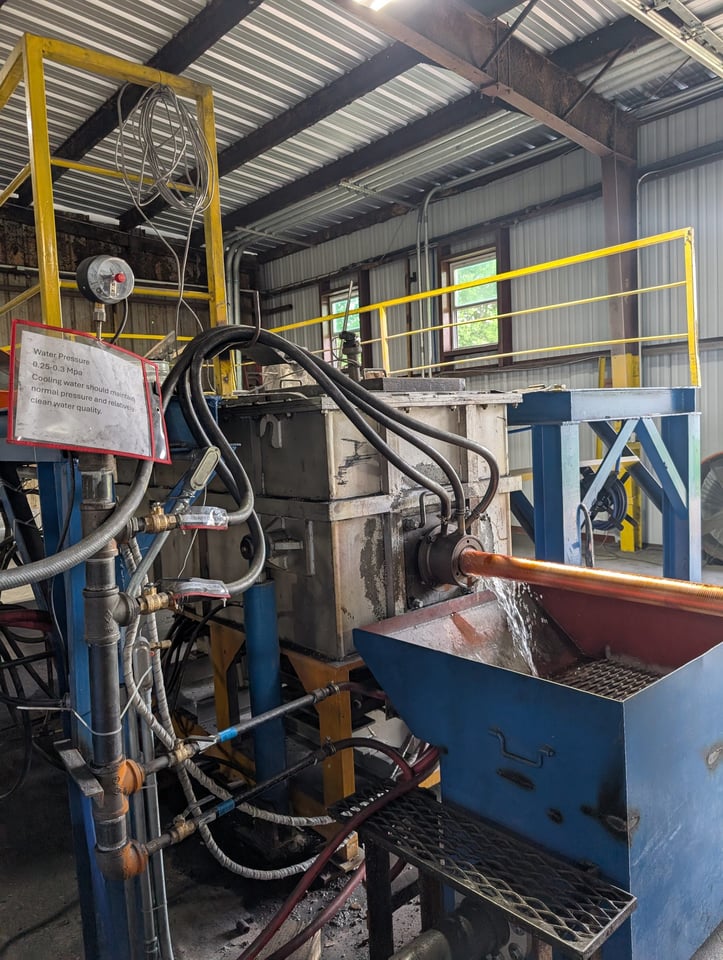
1. Melt
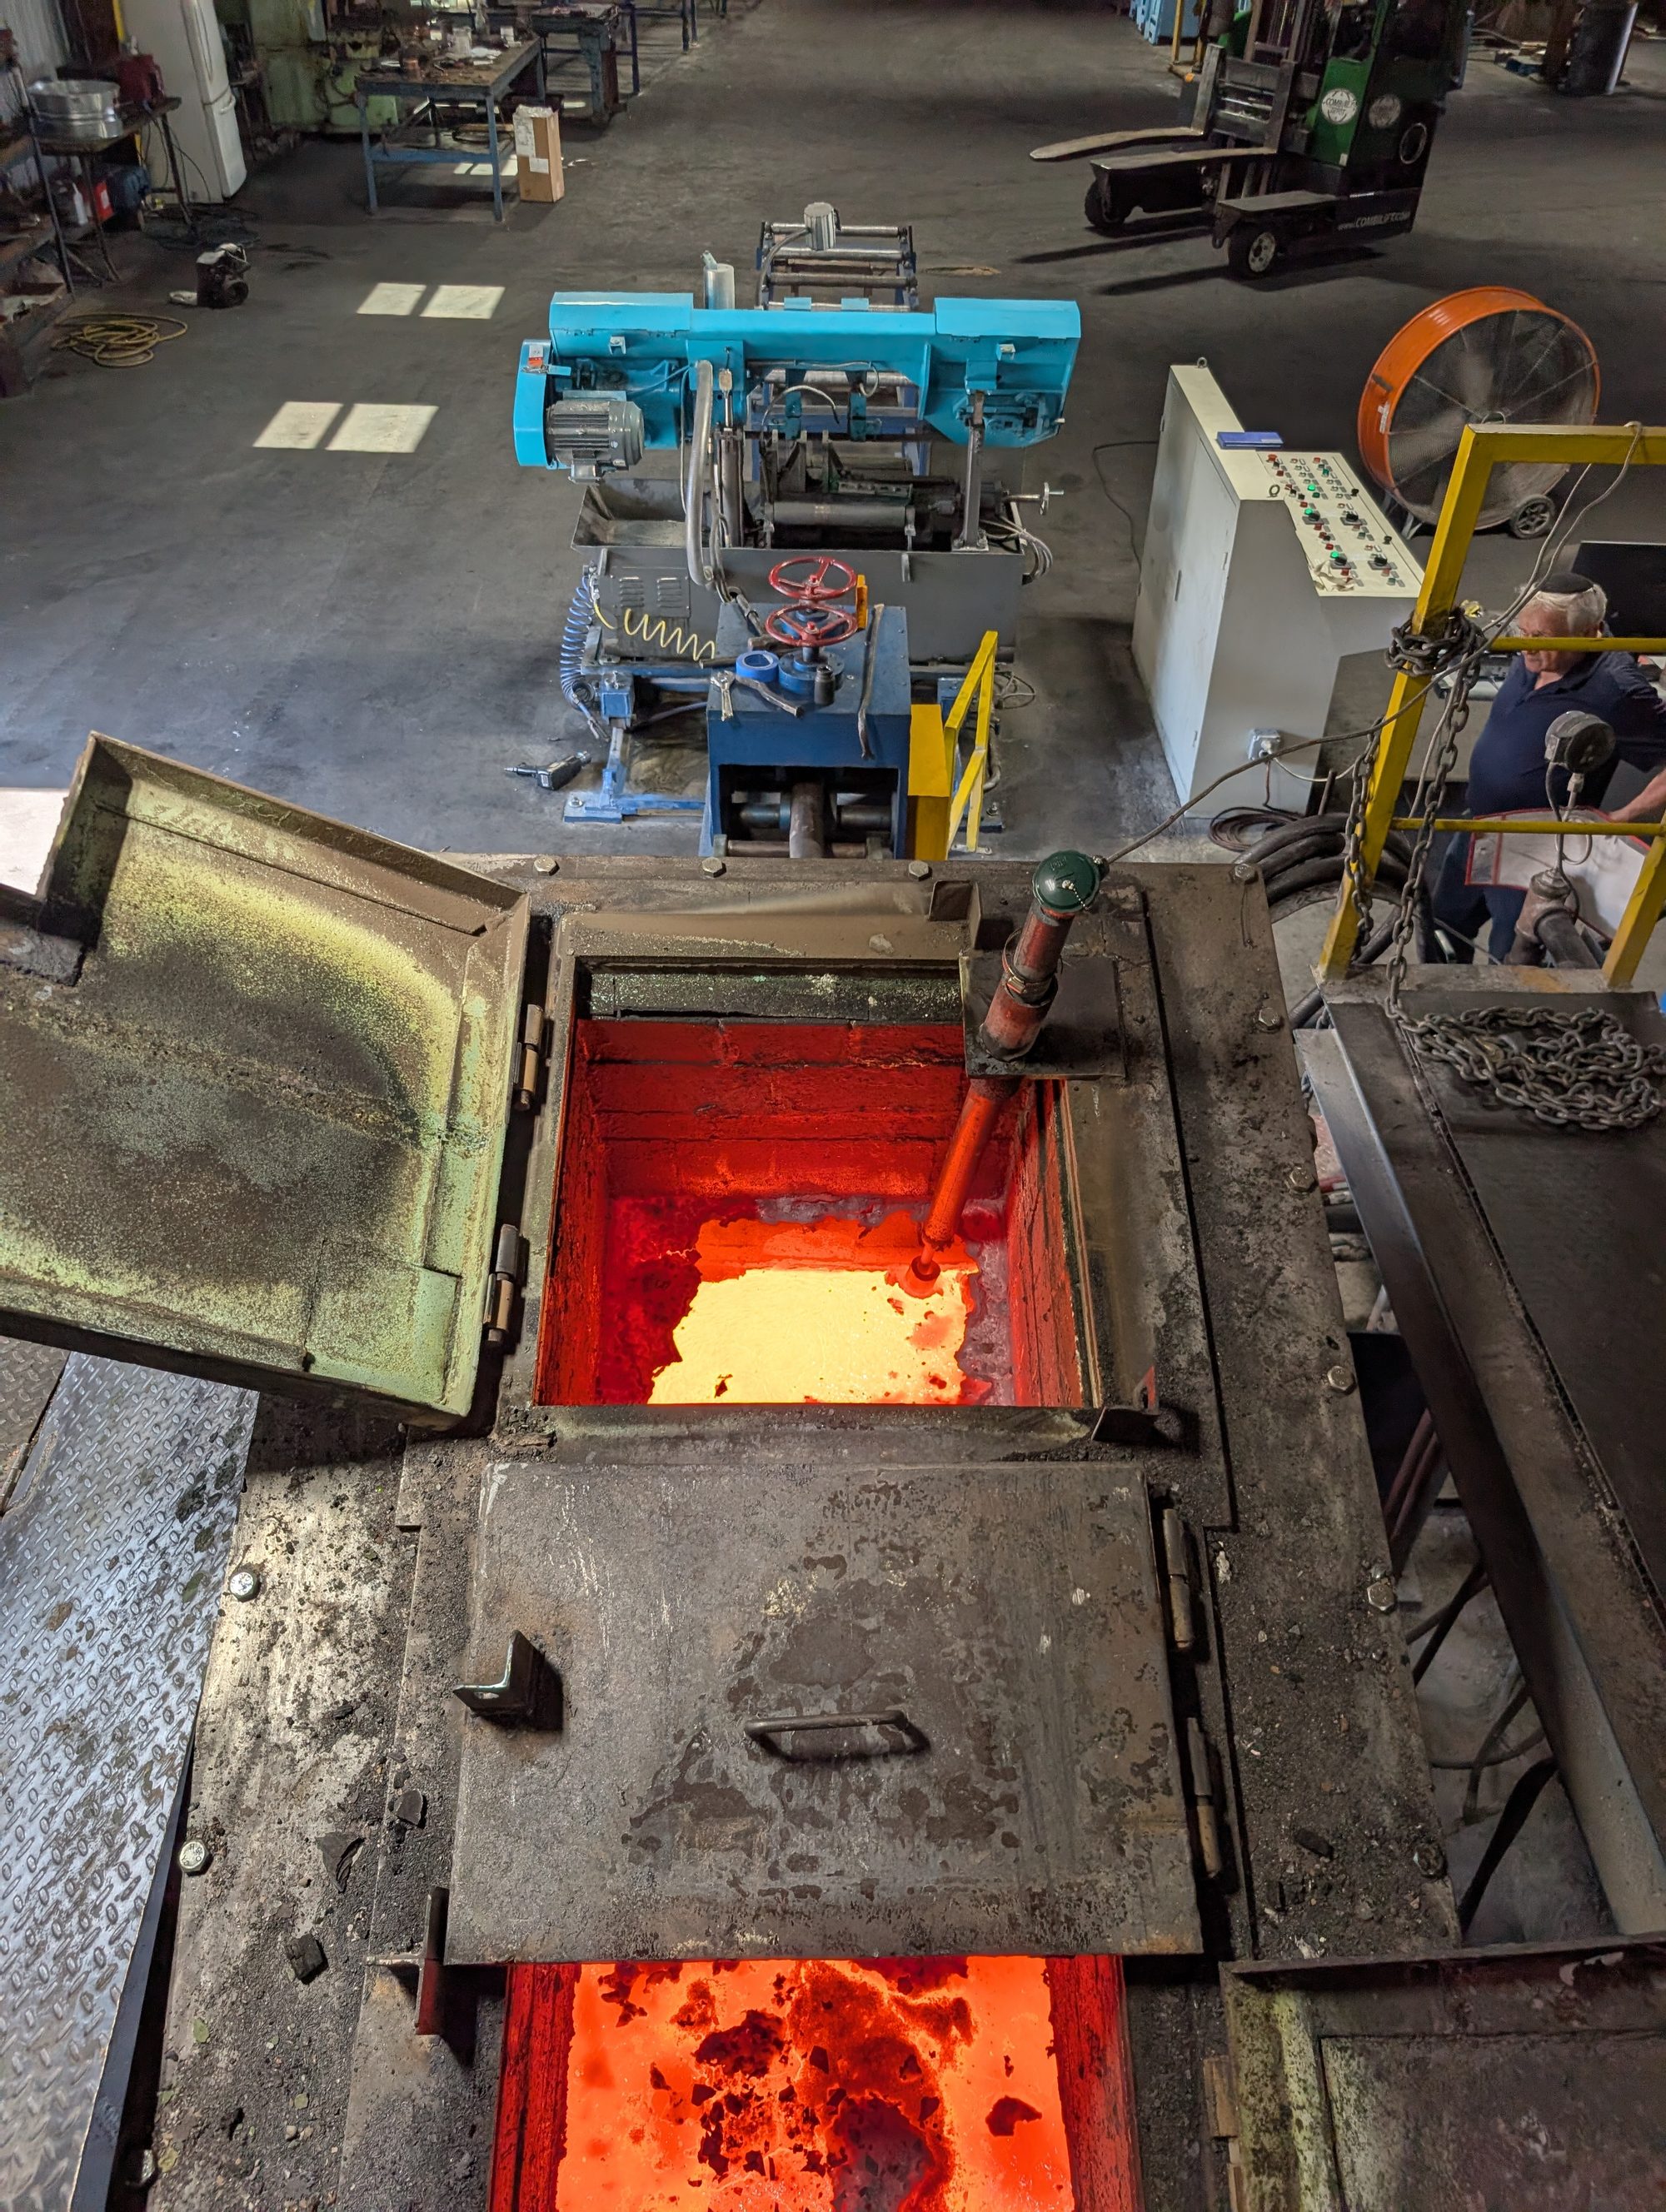
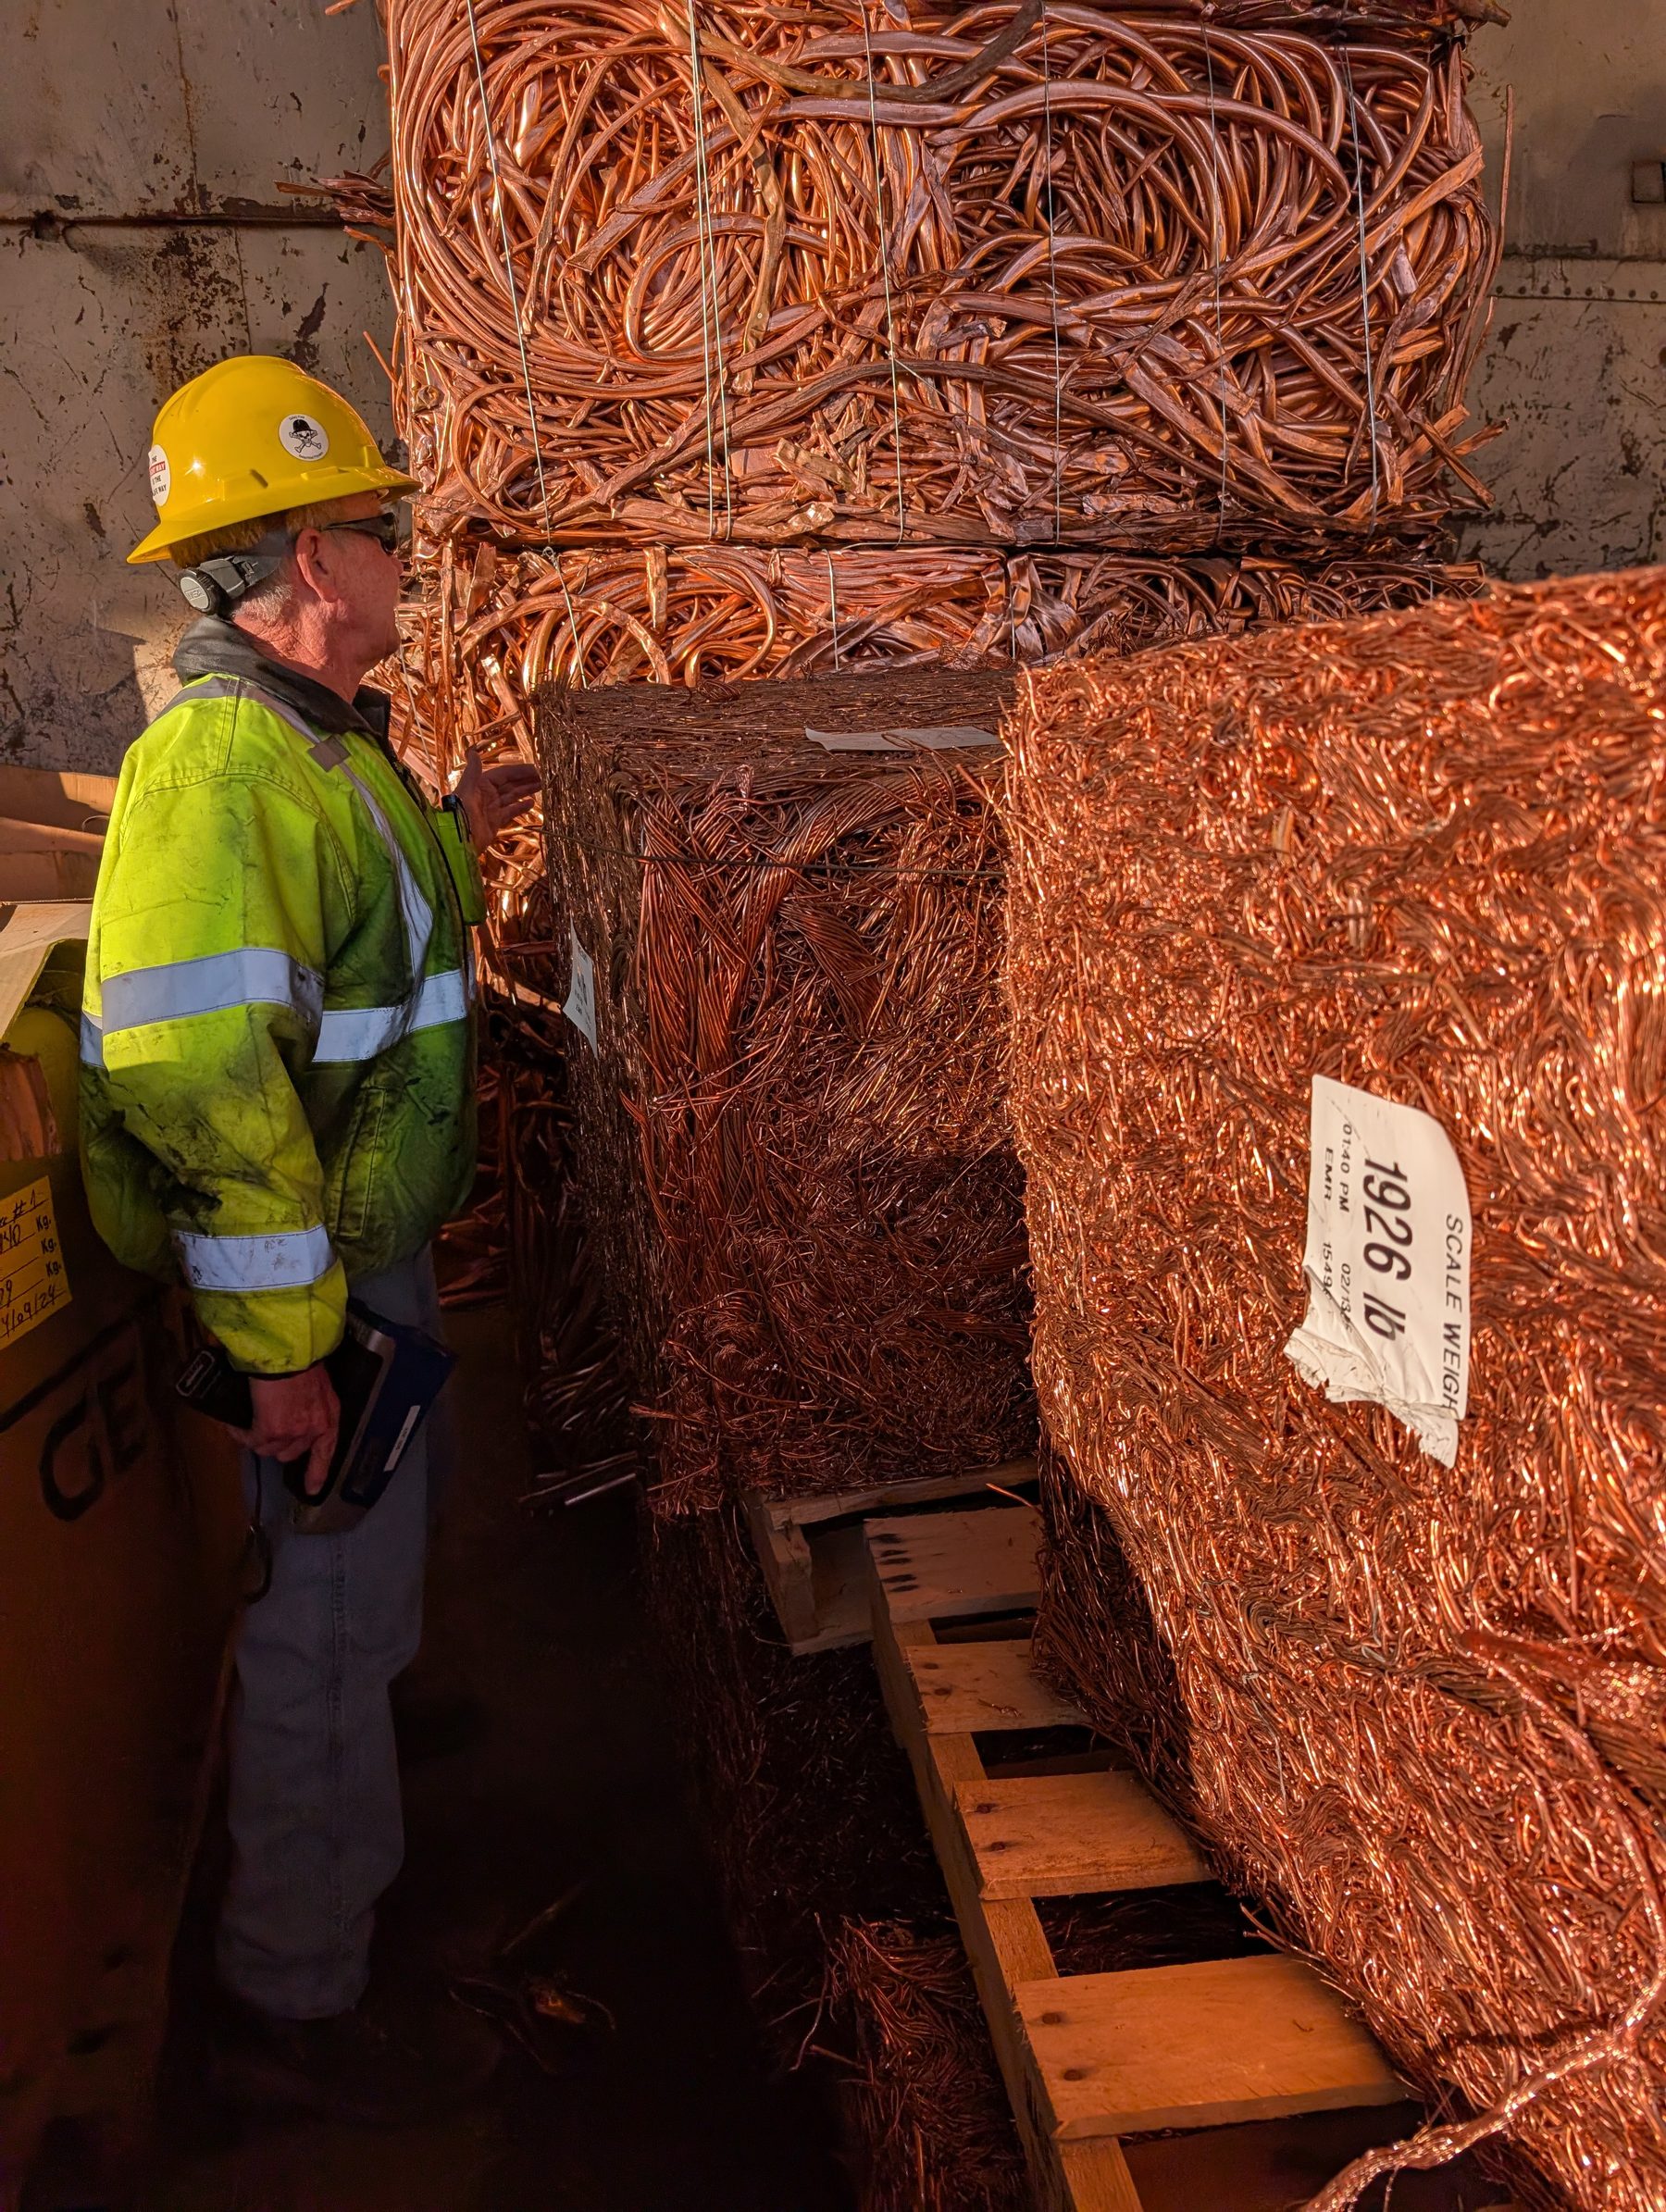
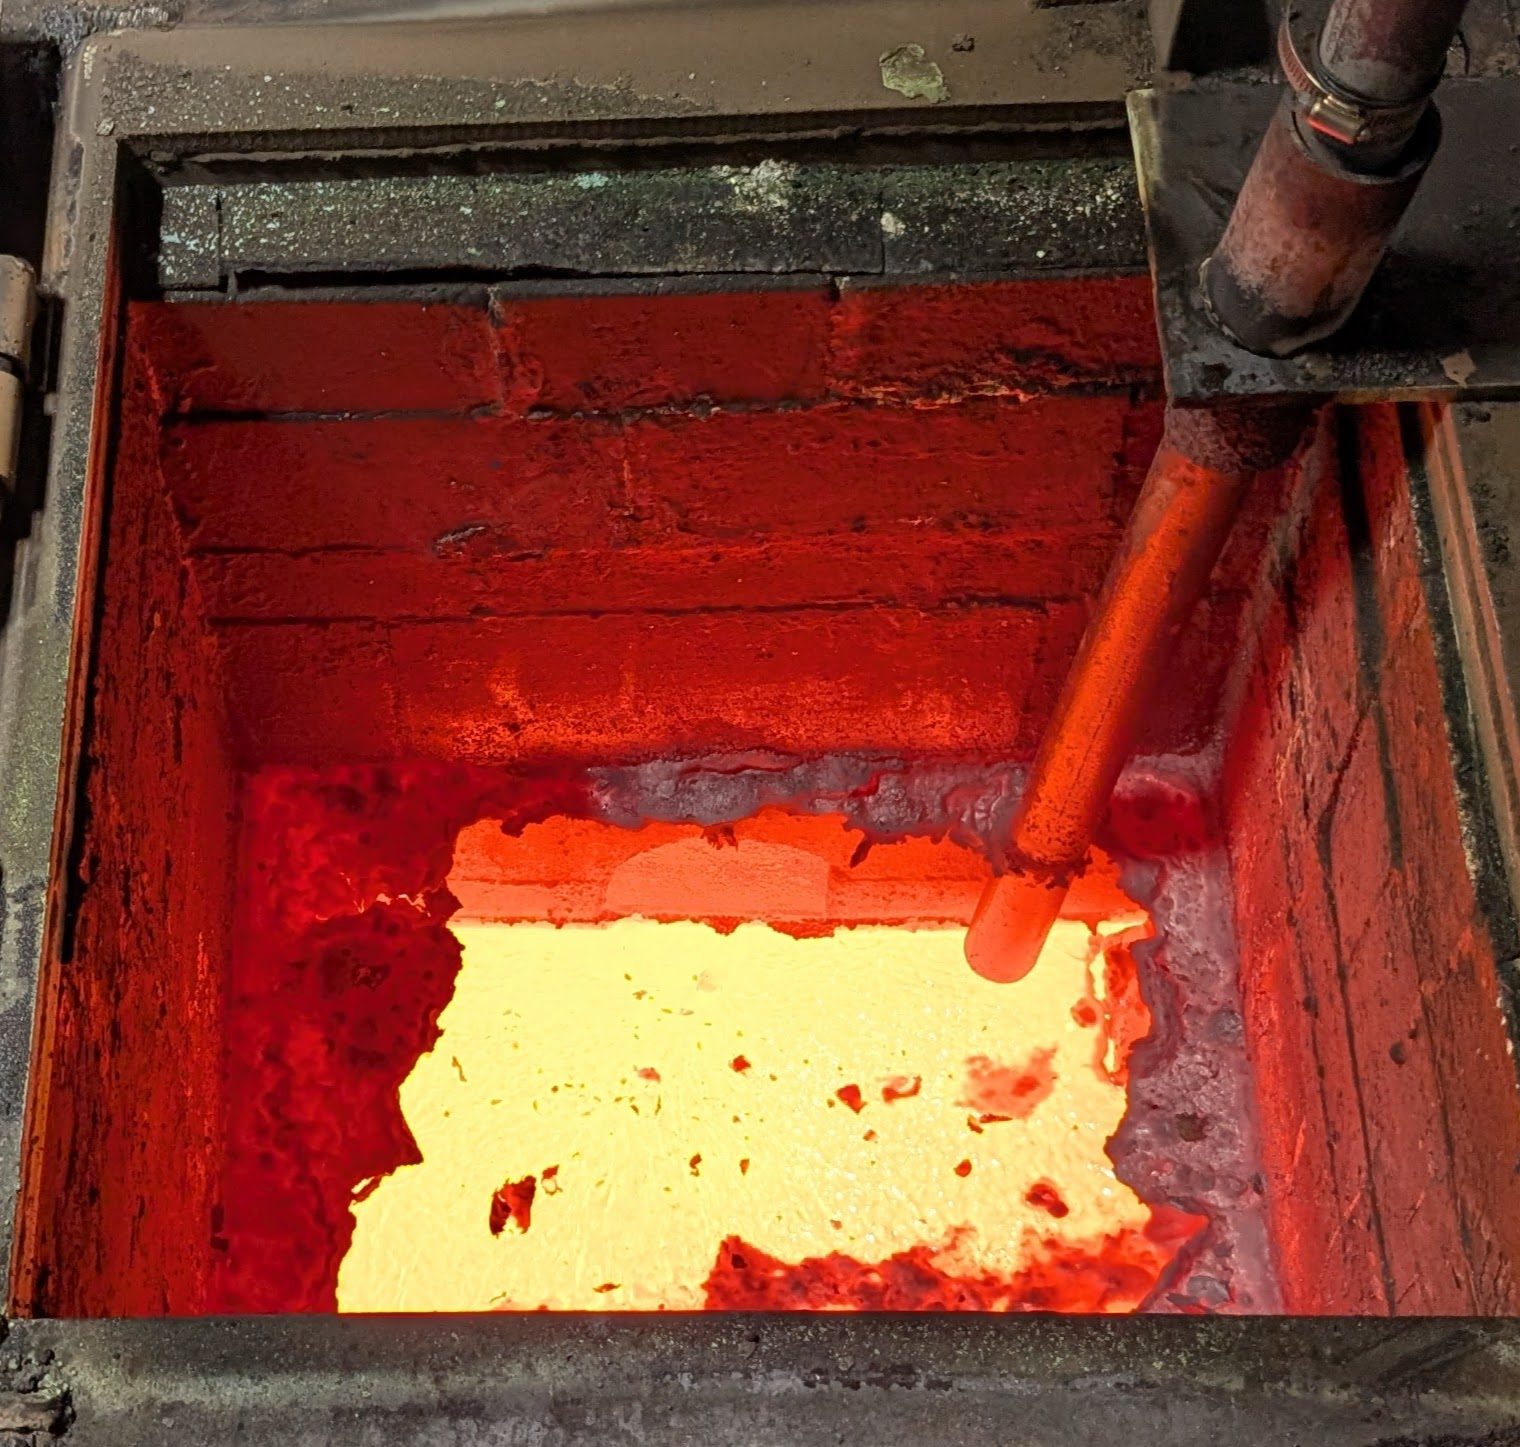
Cathode copper, nickel, zinc, tin, and the minor alloying elements are charged and melted to the target chemistry for the alloy being run: C12200 DHP copper, C23000 red brass, C44300 admiralty, C68700 aluminum brass, C70600 and C71500 copper-nickel, C72200. Chemistry is checked before the pour, and the heat number assigned here follows the tube through every step and onto your mill test report.
New in 2025: melting and casting moved in-house, making Ameritube a fully integrated copper tube mill.
2. Cast
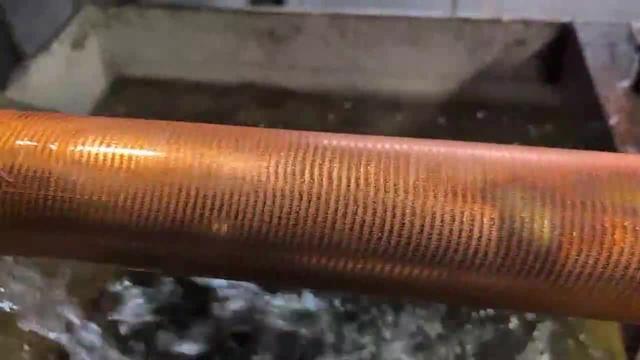
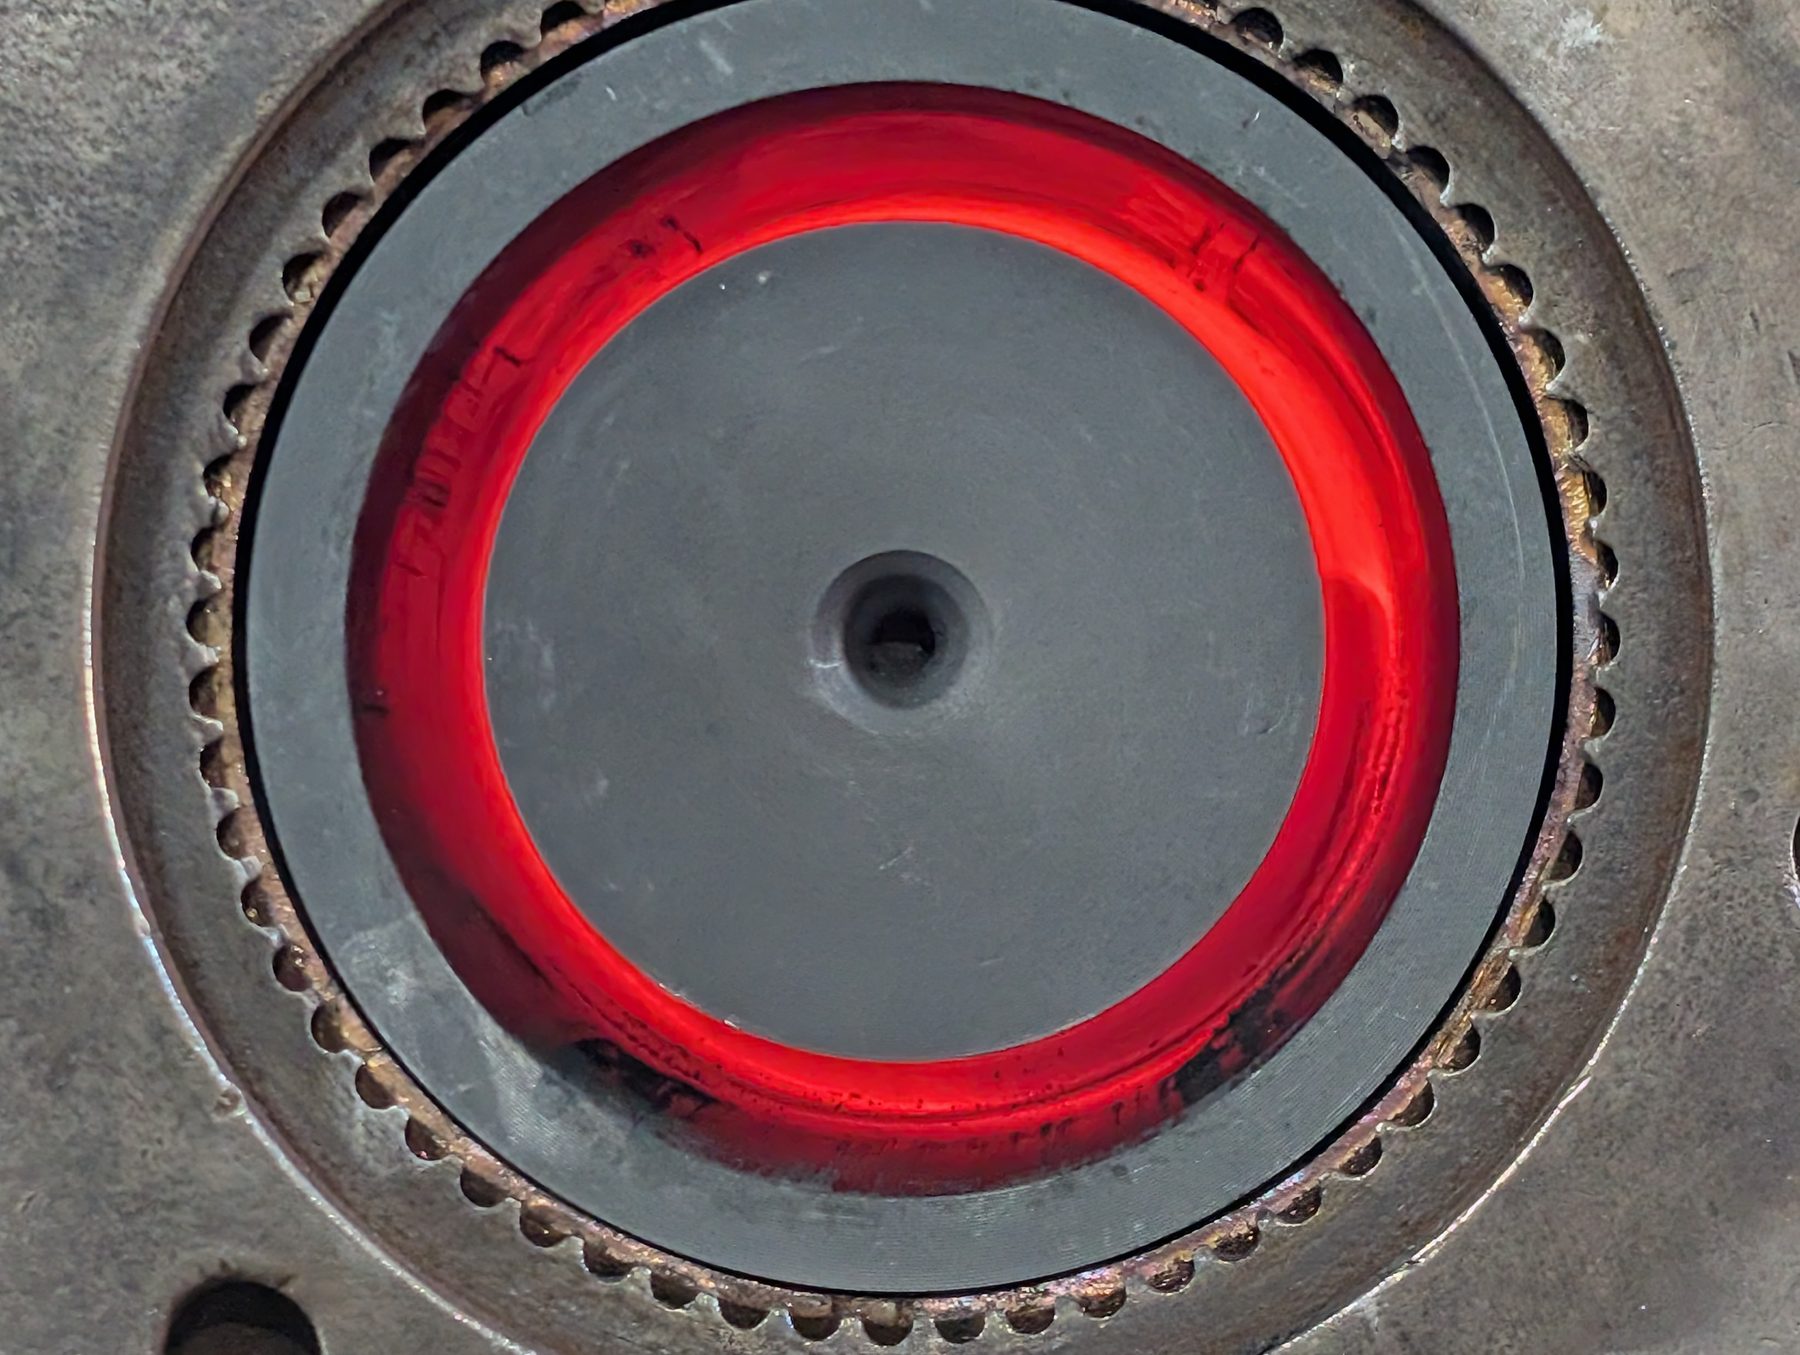
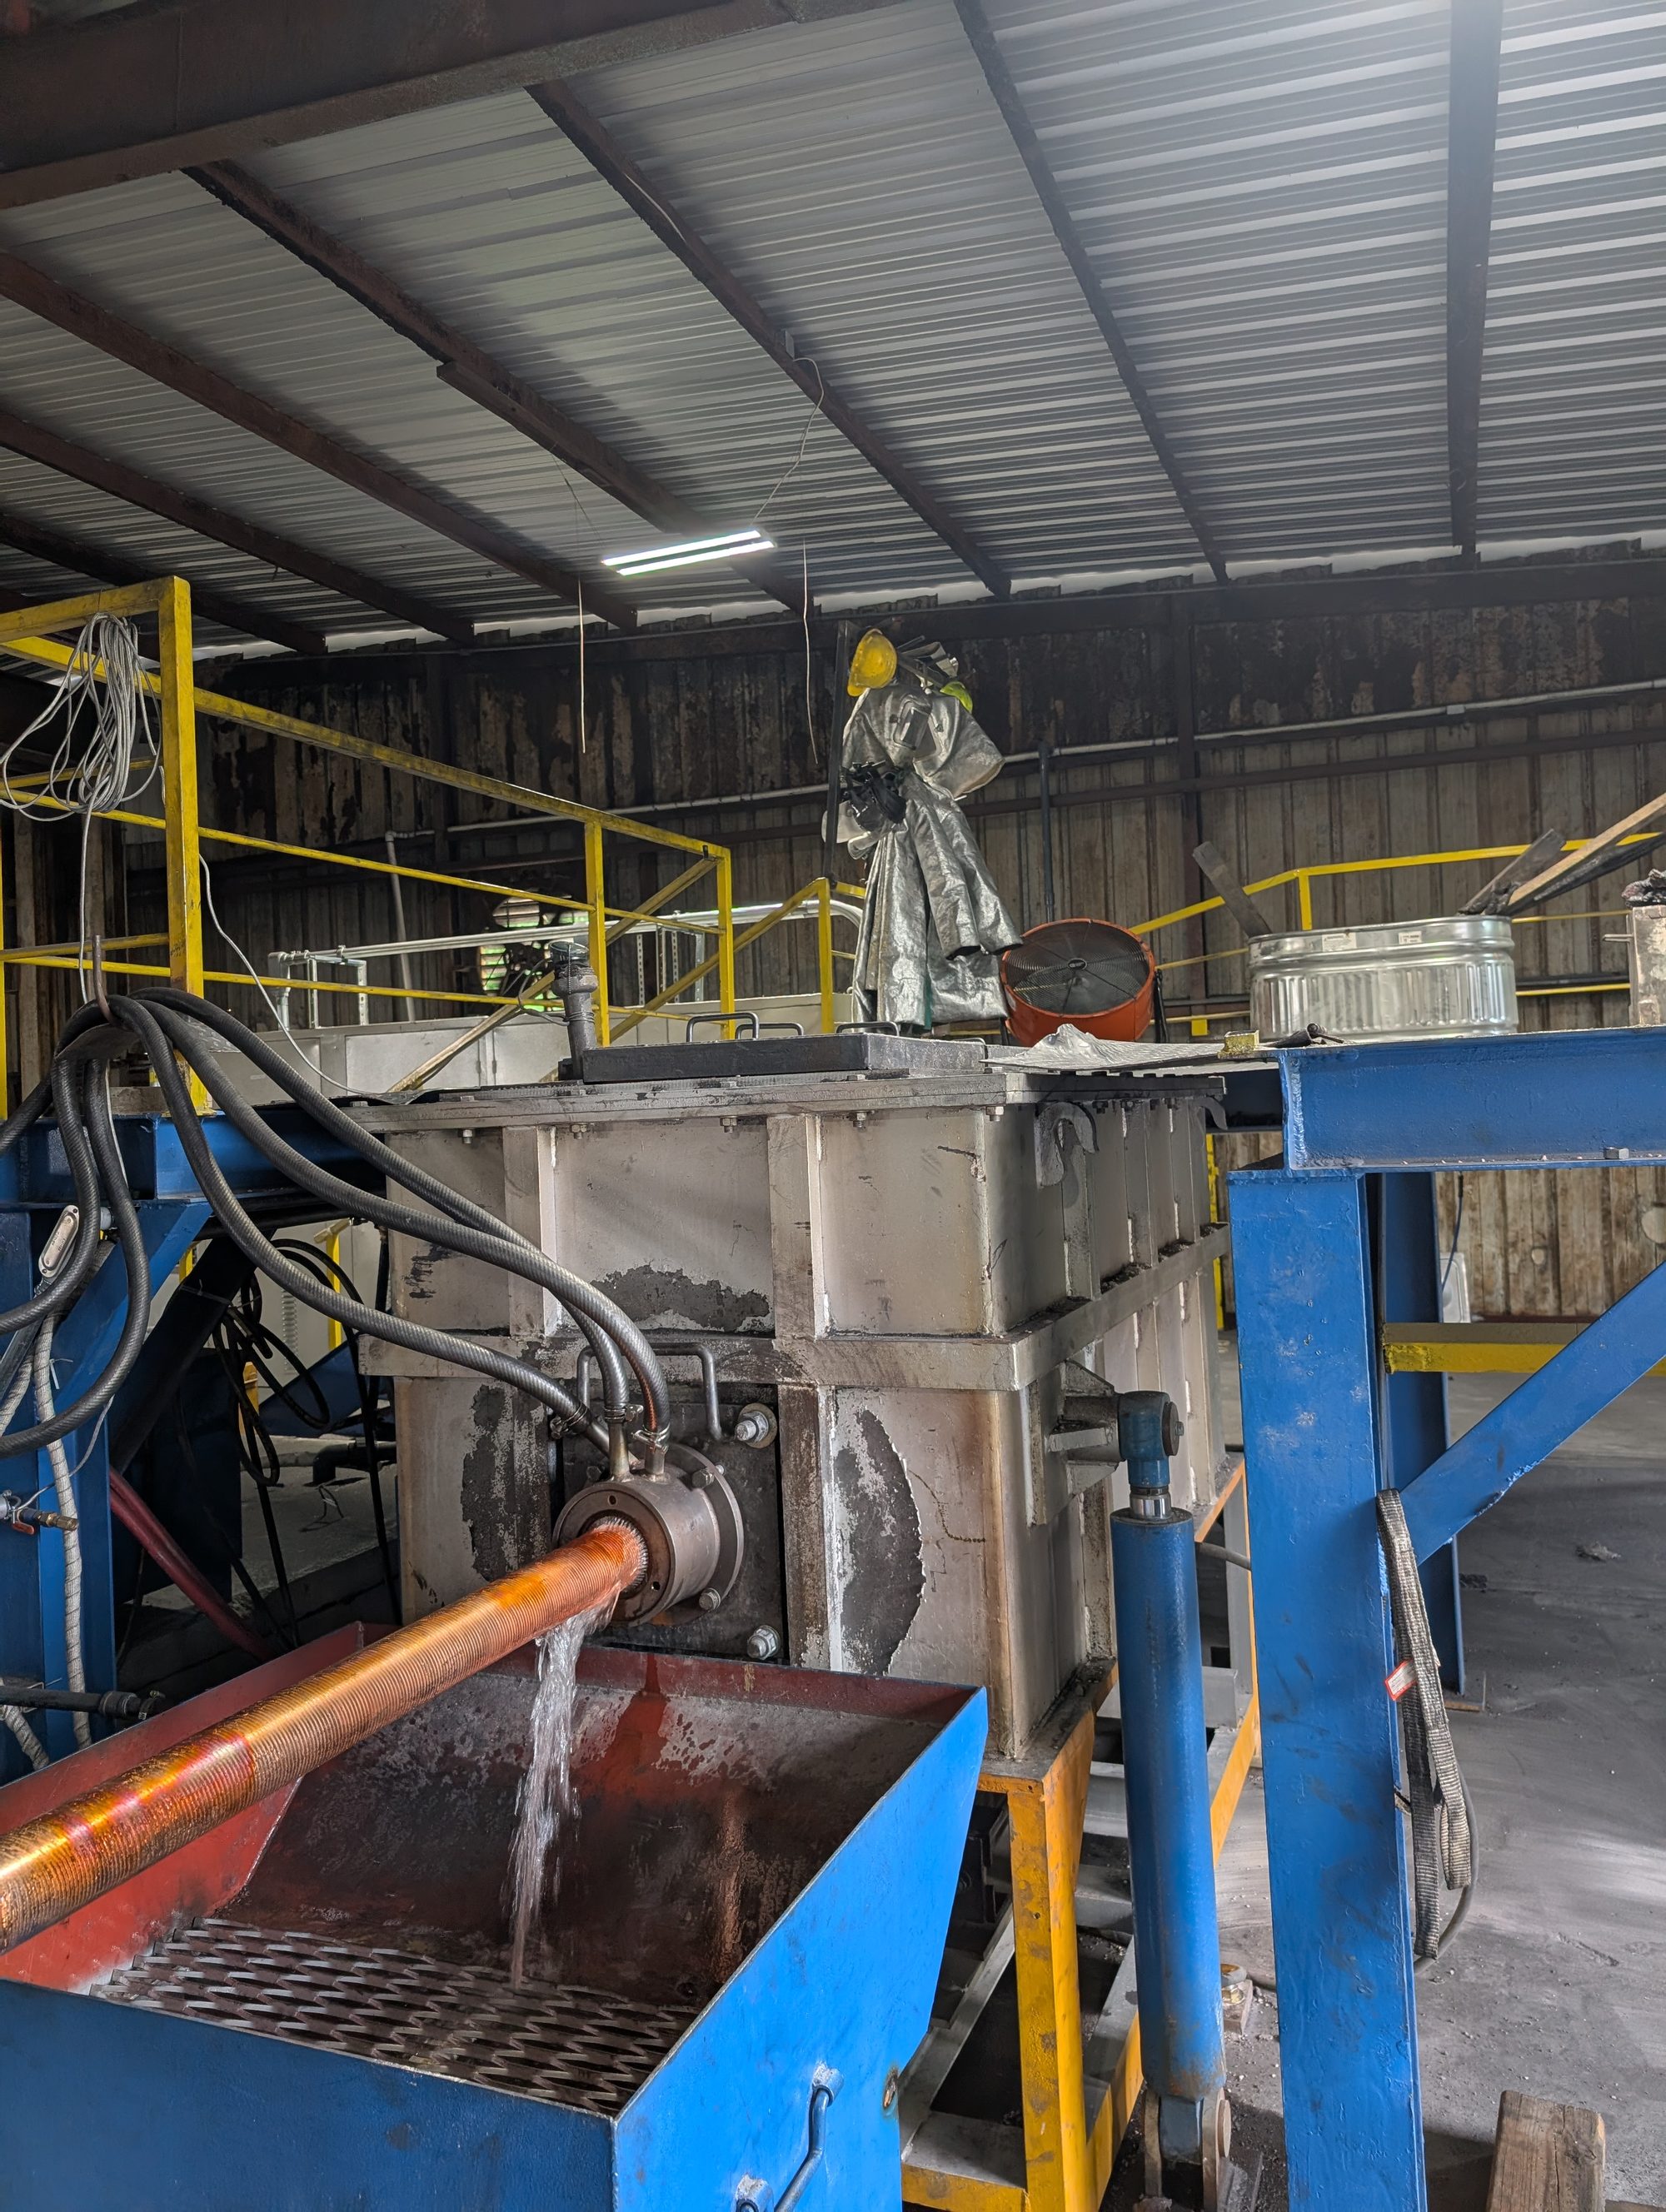
The melt is continuously cast into seamless hollow shells sized for the pilger mill. Casting our own shells means no dependence on foreign hollow suppliers, no customs delays, and no question about where the metal came from. For defense, marine, and federally funded water work, that is the "melted in the USA" line item.
3. Pilger
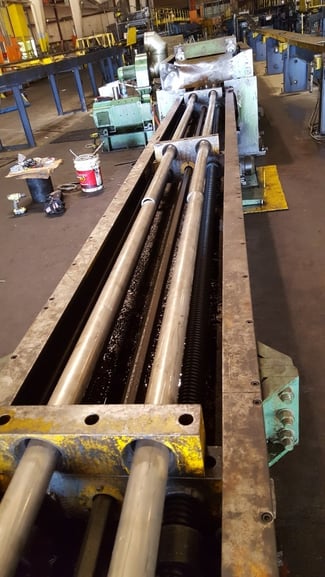
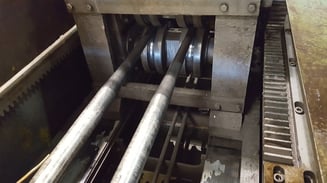
Cold pilger rolling reduces the cast shell's diameter and wall in a single pass while working the grain structure. The pilger mill, installed in 2011, gives us large reductions with excellent wall concentricity, setting up the tube for drawing.
4. Draw 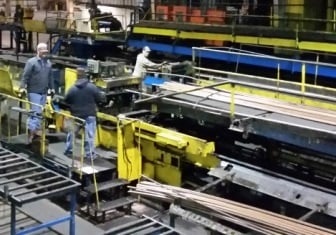
Multi-pass cold drawing on our draw benches brings the tube to finished OD and wall. On demanding alloys such as admiralty brass we run more than 30% reduction per pass. That is deliberate: a hard draw opens up sub-surface defects that a light draw or a tube-sheet roll would never find, so they get caught here rather than in your exchanger. Tungsten carbide dies are polished and maintained in-house.
5. Anneal
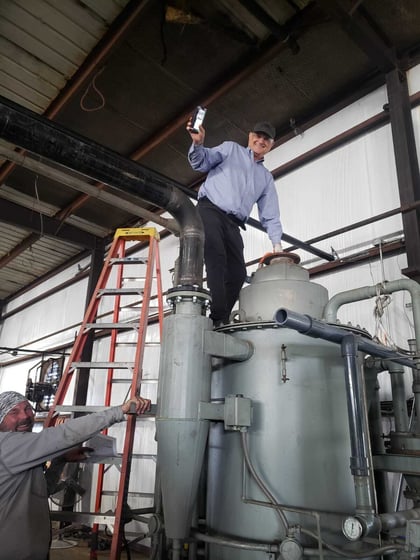
Tube is annealed in our 60-foot controlled-atmosphere furnace to the specified temper: fully annealed (O61), light drawn (H55), or stress relieved between draws. Microstructure and grain size are checked in our lab against SOP-400.
6. Straighten, cut, and finish
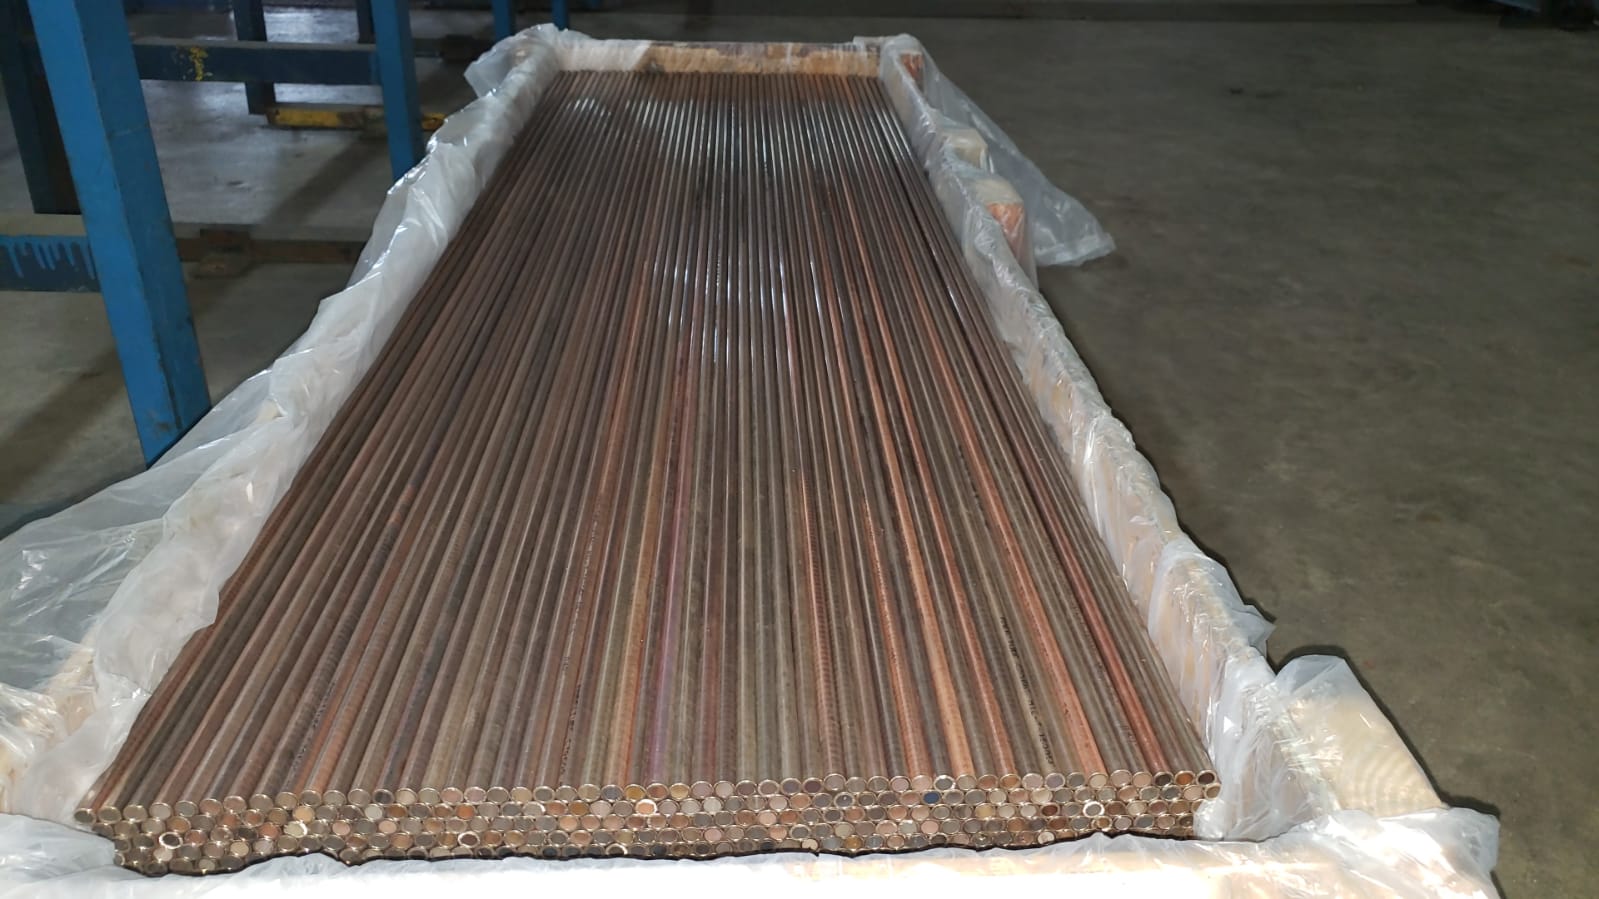
Straightened, cut to length, ends deburred, and cleaned per SOP-903 so the tube arrives ready to roll or braze. Pointing, swaging, bending, and U-bend fabrication are available.
7. Test
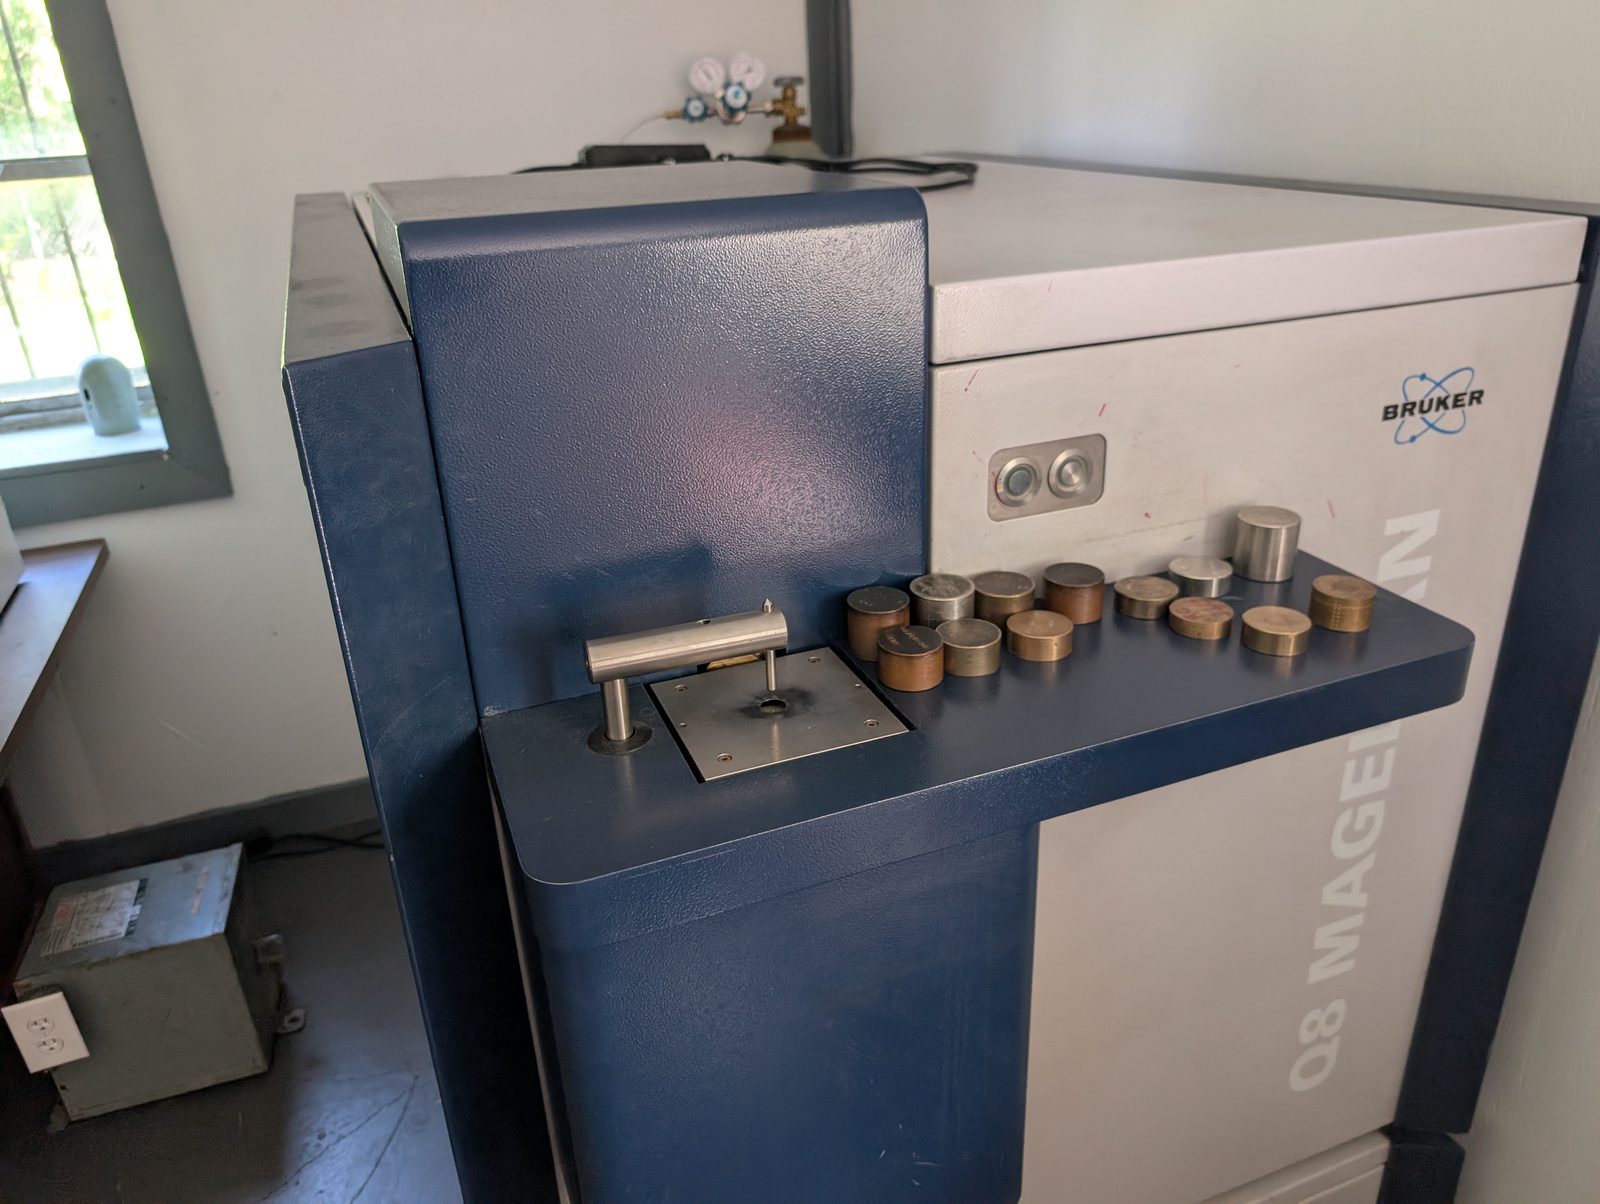
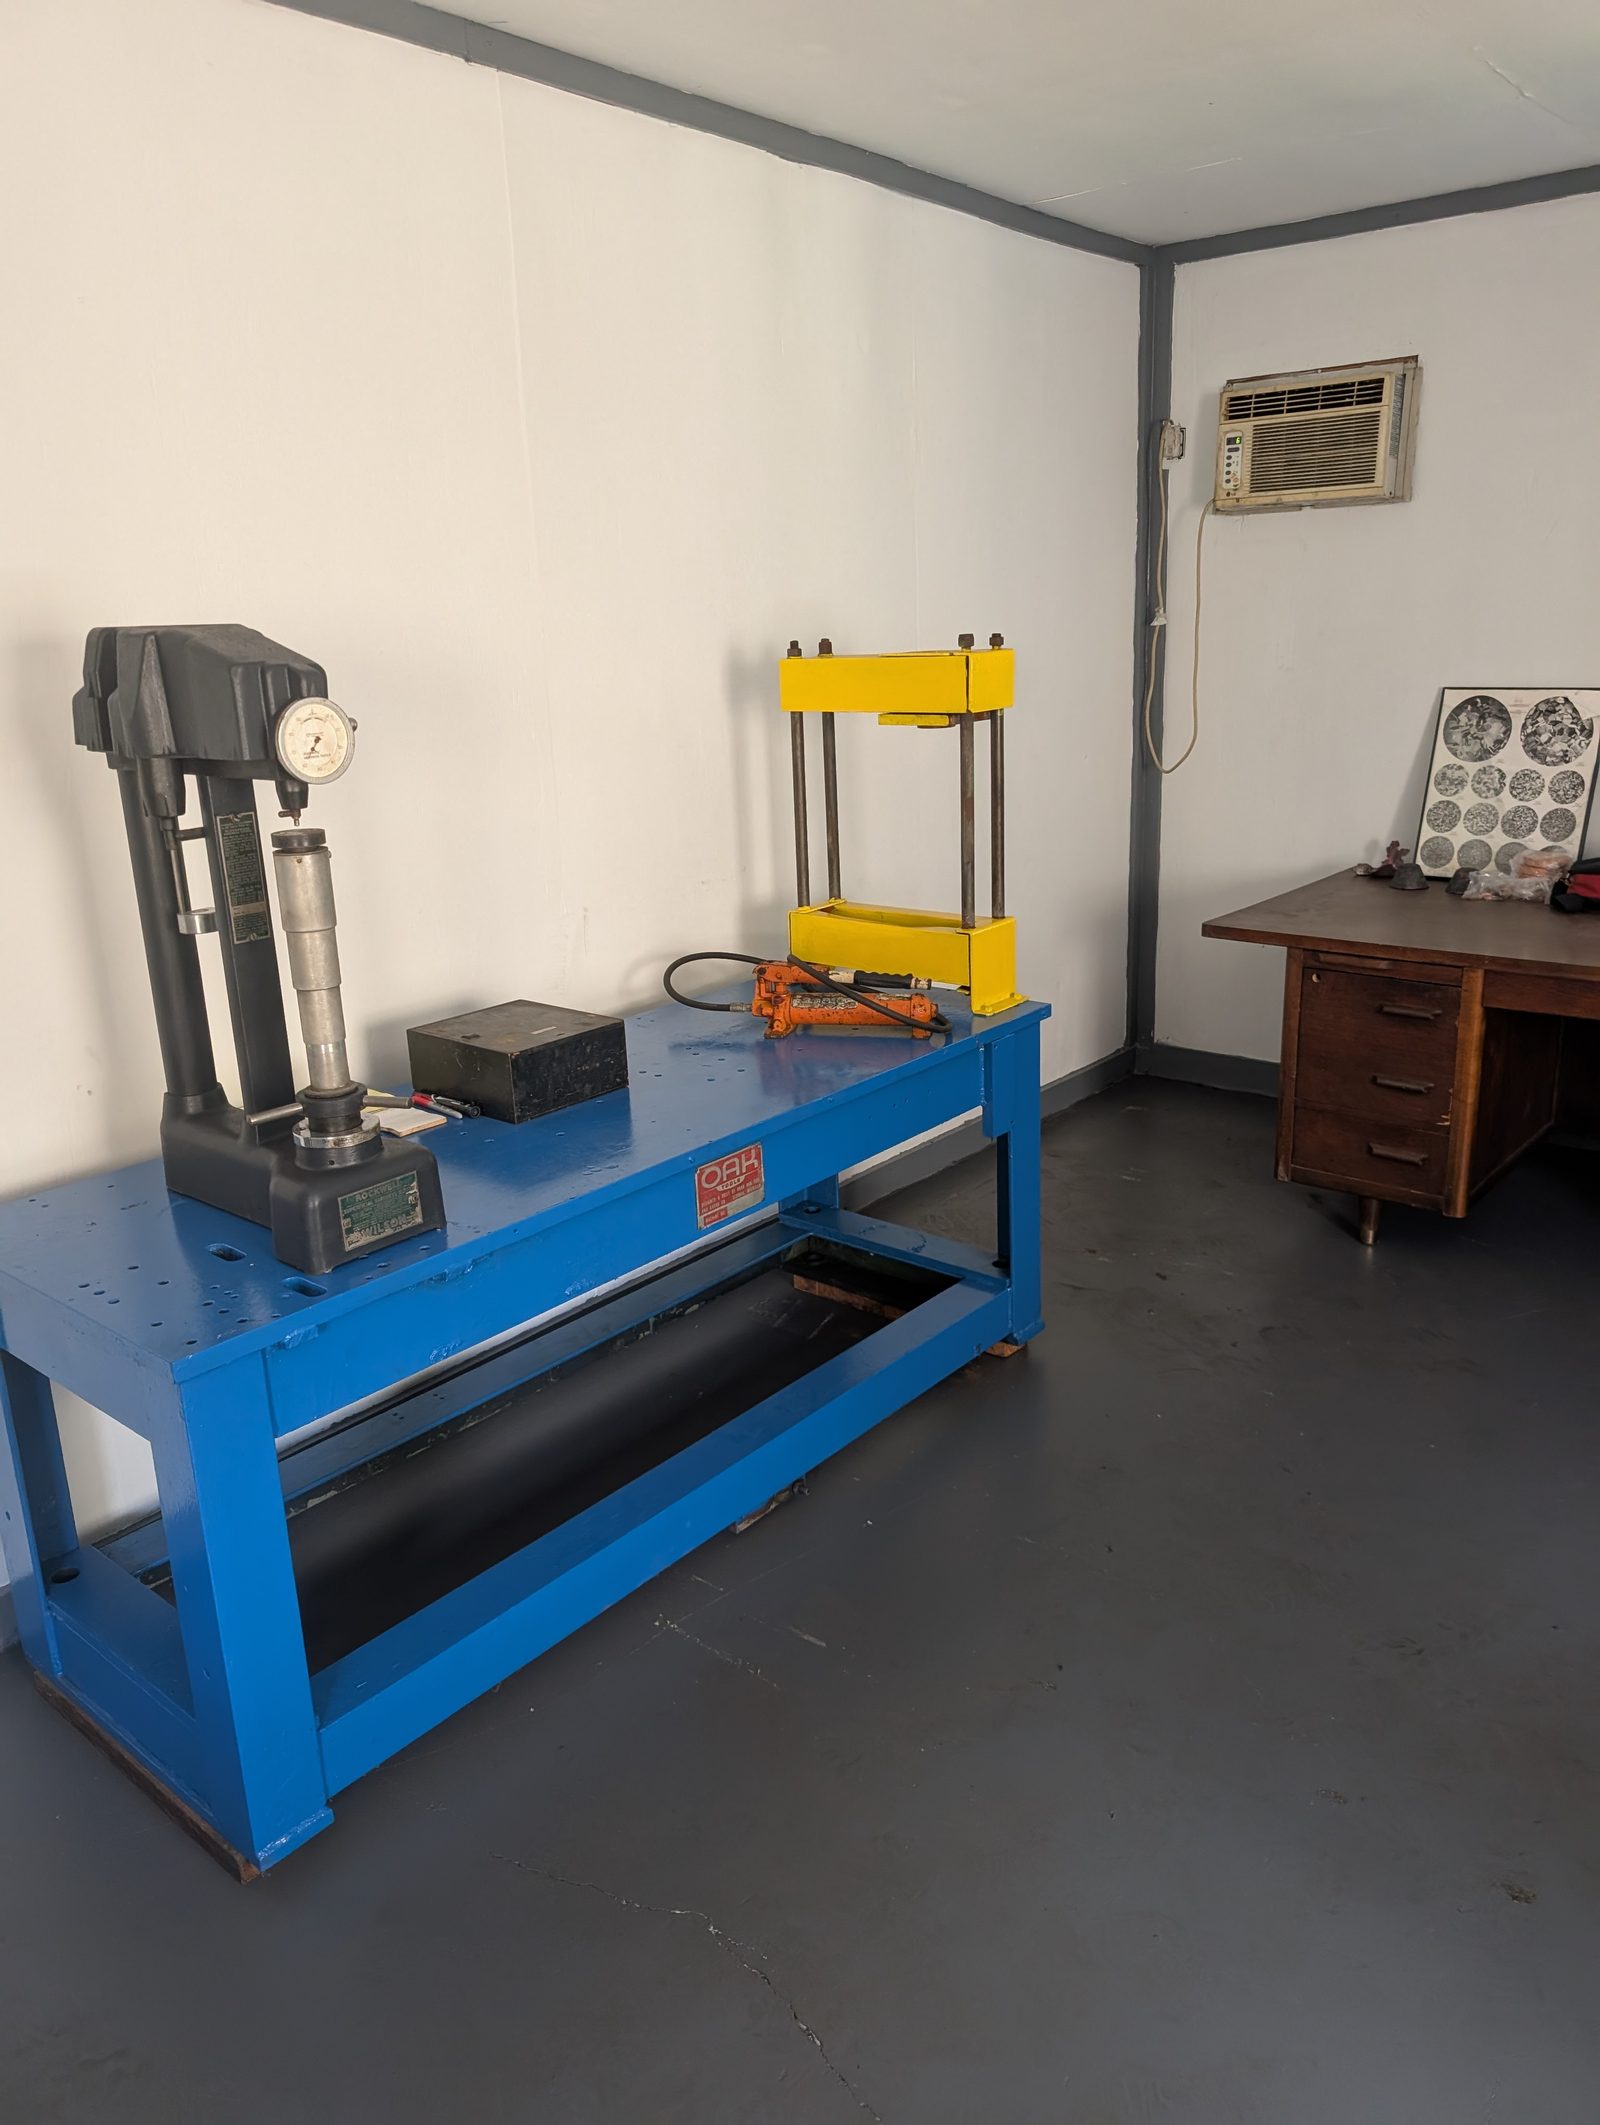
Every tube passes through eddy current inspection. Depending on the specification and your requirements we also perform:
- Hydrostatic testing per SB-111 and MIL-T-16420K
- Air-under-water pneumatic testing
- Ammonia vapor testing for residual stress (SOP-200)
- Ultrasonic testing, in-house and third-party
- Dimensional, hardness, tensile, flare, flatten, and expansion tests
- Microstructure and grain size
NDT is performed by Level II certified operators. Final inspection follows SOP-600, and the results go on the MTR with the chemistry from step one.
Size range
| Range | |
|---|---|
| Copper alloy tube OD | 3/8" to 2-1/2" |
| Wall | .035" to .220" |
| Copper-nickel pipe, manufactured | 1/4" to 2" NPS |
| Copper-nickel pipe, distributed and certified | 2-1/2" to 24" NPS |
| Lengths | Cut lengths to 48'1", coils on DHP copper |
Distribution, backed by the same lab
Carbon, stainless, duplex, and nickel alloy tube is sourced from qualified domestic and international mills, received under SOP-1001, and inspected and released through the same lab and quality system as our own copper. When we distribute it, we can also test it.